Language:


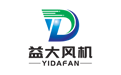
HVOF spraying accelerates tungsten carbide particles to high velocity so that they form a dense coating. Heat input is low and bond strength is high, which suits high velocity fine particle erosion and makes it the least distorting of the common wear processes.
Erosion rate rises roughly with the 2.5 to 3 power of velocity, so coating is concentrated where gas velocity is highest.
| Location | Process | Typical figure |
| Blade leading edge | HVOF tungsten carbide coating | Typical coating hardness HV 1000-1400 |
| Impeller front plate | Local or full coating | Bond strength not lower than 70 MPa |
| High velocity casing area | Coating with sealing treatment | Controls fine particle erosion |
| Inlet cone | Coating or ceramic composite | Selected by erosion severity |
| Shaft and fits | Not coated | Preserves dimensional accuracy |
| Location | Process | Typical figure |
| Surface preparation | Grit blasting to specified cleanliness and roughness | Determines bond strength |
| Spray parameters | Control of gas flow, spray distance and feed rate | Stabilises coating density |
| Thickness control | Thickness set by duty and applied by zone | Balances life and cost |
| Sealing treatment | Sealing of porosity | Limits penetration by corrosive media |
| Bond strength specimen | Pull-off test per GB/T 8642 | Coating acceptance basis |
Applications include dust laden flue gas, catalytic cracking flue gas, metallurgical waste heat and coal or biomass fired boilers.
Coating life depends strongly on particle hardness and impact angle, so the scheme should be set from measured medium data.
Local coating damage can be repaired by re-spraying during maintenance, and repairability should be written into the maintenance plan to avoid replacing the whole rotor.
| Standard | Title | Purpose |
| GB/T 8642 | Thermal spraying - Determination of tensile adhesive strength | Coating bond strength acceptance |
| ASTM G76 | Standard test method for conducting erosion tests by solid particle impingement using gas jets | Erosion wear evaluation |
| GB/T 4340.1 | Metallic materials - Vickers hardness test - Part 1 | Coating and hardened layer hardness |
| GB/T 9239.1 / ISO 21940-11 | Mechanical vibration - Balance quality requirements for rigid rotors | Impeller balancing grade |
| GB/T 1236 | Industrial fans - Performance testing using standardized airways | Air flow, pressure and efficiency testing |
Please provide particle size and hardness, inlet velocity, medium temperature and air flow. Size and motor power are calculated for the actual duty.
Where particles are coarse and abrasive wear dominates, hardfacing is more economical. Where particles are fine, velocity is high and erosion dominates, tungsten carbide spraying is the better fit. Spraying has low heat input, so it suits impellers with tight dimensional requirements.
Detachment usually follows inadequate surface preparation or excessive thickness creating stress concentration. Blast cleanliness, roughness and spray parameters all follow a written procedure and are verified by a bond strength specimen.
Thickness is set from wear rate and inspection interval. Too thin fails early and too thick increases stress and cost, so thickness is specified by zone in the process document and checked by sampling.
Related pages: Wear-resistant fan range Wear-resistant centrifugal fan Dust collection and wear protection
Contact: Lee
Phone: 13793313126
Tel: 0533-6820280
Email: chuanyi99@126.com
Add: Wujia Industrial Park, Nanjiao Town, Zhoucun District, Zibo City, Shandong Province, China